REQUEST A FREE ESTIMATE!
Conveyors for the Canned Food Industry and Their Applications
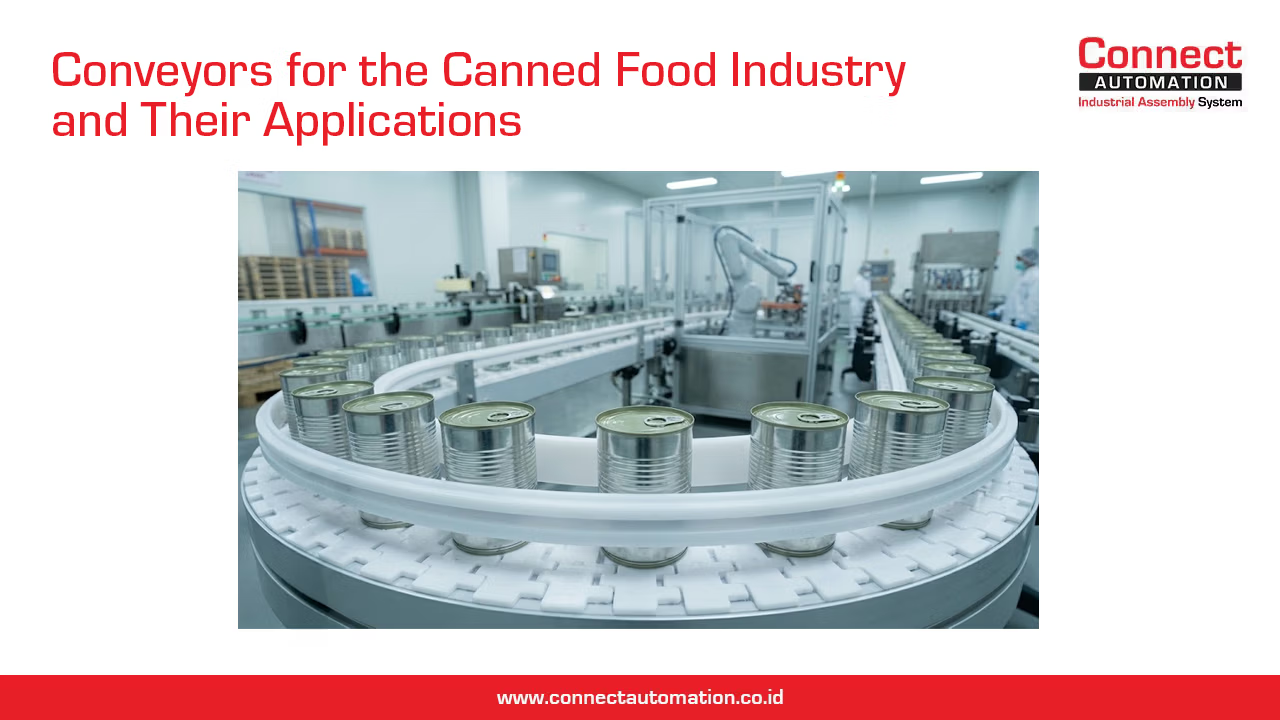
The canned food industry relies on a series of production processes that require products to move consistently from one stage to another. From filling and can seaming to sterilization, cooling, inspection, and further processing, conveyors play an important role in maintaining a continuous and organized production flow.
Canned products can range from sardines, corned beef, canned fruits and vegetables, and condensed milk to ready-to-eat meals and canned beverages. Although these products use similar containers, each production process can have different requirements.
For this reason, choosing a conveyor for the canned food industry requires consideration of the product characteristics, production stage, line speed, operating environment, and hygiene requirements. Table Top Chain Conveyors, Belt Conveyors with PU food-grade belts, and Modular Belt Conveyors with food-grade modular belts can each be used according to the requirements of the production process.
The Canned Food Industry and Its Conveyor Requirements
In a canned food production line, conveyors connect different machines and processing stages, allowing products to move continuously throughout the production process. The conveyor system may handle both empty cans and cans that have already been filled with products. Common canned food products include:
- Fish products such as sardines and tuna
- Corned beef and other canned meat products
- Canned fruits and vegetables
- Condensed milk and certain dairy products
- Ready-to-eat canned meals
- Canned beverages such as coffee, tea, soft drinks, and energy drinks
Differences in can size, product weight, surface condition, and processing requirements mean that each production line may require a different conveyor configuration. A conveyor transporting empty cans toward a filling machine, for example, may have different requirements from a conveyor handling filled cans after the filling and seaming processes.
Production Stages That Use Conveyors
Conveyors can be integrated into various stages of a canned food production line. A typical process may include:
Product Preparation → Filling → Seaming → Sterilization/Retort → Cooling → Inspection → Labeling → Packing
At each stage, the conveyor serves a different purpose.
1. Transferring Cans to the Filling Machine
Before filling process, empty cans need to be transferred to the filling machine with controlled positioning and spacing. Table Top Chain Conveyors are commonly suitable for applications where cans need to remain upright while moving continuously along the production line.
2. After Filling and Seaming
Once the product has been filled into the can, the can moves toward the seaming process and subsequent production stages. The conveyor needs to provide stable product movement while maintaining a consistent connection between machines.
3. Sterilization and Cooling
Canned food production can involve high temperatures, water, steam, and cooling processes. These conditions make conveyor material an important consideration, particularly in areas exposed to moisture and regular cleaning.
4. Inspection and Quality Control
After the main processing stages, cans may pass through inspection areas to check product and container conditions. The conveyor provides a consistent product flow through the inspection point.
Table Top Chain Conveyors for the Canned Food Industry
Table Top Chain Conveyor is one of the commonly considered conveyor solutions for rigid products such as cans. Its continuous chain surface provides a stable path for transferring products between different production stages.
For the canned food industry, Table Top Chain Conveyors can be configured with different chain materials depending on the application.
1. Stainless Steel Table Top Chain
Stainless steel Table Top Chain can be selected for applications that require good mechanical durability and resistance to certain production environments. It can be suitable for areas where the chain needs to withstand continuous operation and specific operating conditions.
2. Brown Plastic Table Top Chain
Plastic Table Top Chain can also be used for canned food applications where the production conditions are suitable. Its lighter construction provides an alternative to stainless steel chain. The selection should consider factors such as can size and weight, conveyor speed, operating environment, and production requirements.
3. White Plastic or Hygienic Table Top Chain
For production areas with higher hygiene requirements, white plastic or hygienic Table Top Chain can be considered. This type of configuration is commonly associated with hygienic conveyor systems used in food and beverage production, as well as other industries where conveyor hygiene is an important consideration.
The choice should not be based on chain color alone. Material, construction, specifications, and the actual operating conditions should all be considered when selecting the appropriate chain.
Stainless Steel Frames for Table Top Chain Conveyors
The conveyor frame is another important component of a canned food production system. Food production environments can involve water, humidity, cleaning processes, cooling, and product residues. For this reason, stainless steel frames are widely considered for conveyor systems installed in food production areas.
Stainless steel provides good corrosion resistance and can support easier cleaning and maintenance compared with materials that are less suitable for these environments.
Belt Conveyors for the Canned Food Industry
Belt Conveyors can also be used at specific stages of a canned food production line. For food processing applications, the belt material needs to be selected according to the requirements of the production environment. One suitable option is a PU food-grade belt.
PU Food-Grade Belt
A PU food-grade belt provides a continuous conveying surface for transferring products through various production stages. Belt Conveyors can be considered when the product characteristics or production process are better suited to a continuous belt surface than a chain conveyor.
Some factors to consider include:
- Product size and weight
- Conveyor speed
- Product condition
- Production stage
- Cleaning requirements
- Production line layout
Stainless Steel Frames for Belt Conveyors
For canned food production environments, a Belt Conveyor can be designed using the combination of:
PU food-grade belt + stainless steel frame
This combination provides a conveying surface suitable for food processing applications while using a frame material designed to handle production environments involving water, humidity, and cleaning.
Modular Belt Conveyors for the Canned Food Industry
Modular Belt Conveyors provide another option for canned food production lines. Unlike conventional conveyors that use a continuous belt, Modular Belt Conveyors use interconnected belt modules that form the conveying surface.
Food-Grade Modular Belts
For food applications, the modular belt should be selected based on its food-grade specifications and the requirements of the production process. Modular belts can be considered when the production line requires a modular construction, a particular conveyor configuration, or conveying characteristics that are better suited to this type of belt.
Stainless Steel Frames for Modular Conveyors
As with Table Top Chain and Belt Conveyors, the frame of a Modular Conveyor installed in a food production area can be constructed from stainless steel. The combination of:
food-grade modular belt + stainless steel frame
can provide a conveyor configuration designed around the requirements of the food production environment and the specific process.
Accumulation in Canned Food Production
A canned food production line usually consists of several machines operating in sequence. Each machine may have a different processing capacity and operating speed.
For example:
Filling → Seaming → Sterilization → Inspection
Differences in machine speed can create a need for buffer space or accumulation within the conveyor system.
Accumulation allows a certain number of products to remain within a designated conveyor section while the downstream process adjusts to its available capacity.
In canned food production, accumulation can help:
- Provide a buffer between production stages
- Manage differences in machine speeds
- Maintain an organized product flow
- Support continuous production
- Keep the production line better coordinated during temporary process variations
For this reason, accumulation requirements should be considered during the conveyor design stage.
Why Is Stainless Steel Important for Canned Food Conveyors?
One of the important considerations when designing conveyors for the canned food industry is the production environment. Canned food processing can involve water, steam, cooling, washing, cleaning, and humidity. These conditions make material selection an important part of conveyor design.
Choosing an appropriate frame material helps the conveyor withstand the production environment while supporting regular cleaning and maintenance requirements. This is why stainless steel is widely used for conveyor frames in food production applications.
The appropriate stainless steel grade should also be selected according to the operating conditions, cleaning methods, and production requirements.
Integrating Conveyors with Production Machines
A conveyor in the canned food industry is more than a product transfer system. It forms part of the overall production line and needs to work together with the machines involved in the process.
A simplified production line may look like:
Filling Machine → Conveyor → Seaming Machine → Conveyor → Sterilization → Conveyor → Inspection → Labeling
When designing this type of system, several factors need to be considered:
- Machine height
- Production speed
- Product spacing
- Product transfer
- Accumulation
- Sensors and controls
- Direction changes
- Production environment
Proper integration allows the conveyor system and production machines to work together as one coordinated production line.
Table Top Chain, Belt, or Modular Conveyor?
All three conveyor types can be used in canned food production, but their suitability depends on the specific production stage and operating requirements.
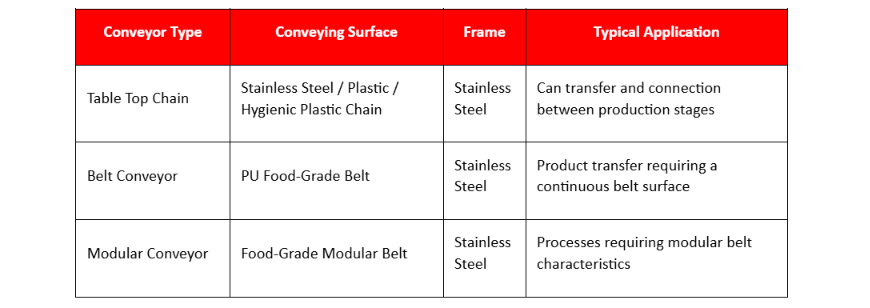
Table Top Chain Conveyor can be a suitable primary solution for many can-handling applications because it provides stable and continuous product movement while connecting different machines within the production line.
Belt Conveyors and Modular Belt Conveyors can also be selected for specific stages where their conveying characteristics are better suited to the product or process. Therefore, conveyor selection should be based on the requirements of each production stage, rather than the type of product alone.
Factors to Consider When Choosing a Conveyor
Before selecting a conveyor for the canned food industry, several factors should be evaluated.
- Can Size and Weight : Can diameter, height, and weight can affect the selection of the chain or belt, conveyor speed, and overall system capacity.
- Product Condition : Empty cans, filled cans, and cans after cooling may require different handling characteristics.
- Production Speed : The required number of cans per minute should be matched with the conveyor capacity and the machines connected to the production line.
- Production Environment : Consider exposure to water, humidity, heat, steam, cleaning processes, and other conditions that may affect conveyor materials.
- Accumulation Requirements : When several machines operate at different speeds, accumulation may become an important part of the conveyor design.
- Production Line Layout : Conveyor length, direction changes, transfers, inclines, and machine positions should be considered during the initial design.
- Conveyor Materials : Materials should be selected according to the requirements of each application, including:
- Stainless steel Table Top Chain
- Plastic Table Top Chain
- Hygienic plastic Table Top Chain
- PU food-grade belt
- Food-grade modular belt
- Stainless steel frame
Conclusion
Conveyors for the canned food industry play an important role in connecting different production stages, from filling and seaming to sterilization, cooling, inspection, and subsequent processes.
Table Top Chain Conveyors can be a primary solution for many can-handling applications, providing stable and continuous product movement throughout the production line. However, Belt Conveyors with PU food-grade belts and Modular Belt Conveyors with food-grade modular belts can also be used for production stages where their characteristics are more suitable.
For food production environments, stainless steel frames are an important consideration across these conveyor types because production lines can involve water, humidity, cleaning, and other demanding operating conditions.
By considering product characteristics, production stages, line speed, accumulation requirements, operating environment, and conveyor materials, a conveyor system can be designed to better support the specific requirements of a canned food production line.
Connect Automation specializes in providing automation solutions, including conveyor systems, to improve efficiency across various industries. The company delivers cutting-edge technology to help organizations automate tasks and optimize workflows. Connect Automation helps businesses reduce manual efforts, boost productivity, and achieve better outcomes. With a customer-focused approach, the company designs tailored solutions to ensure smooth and effective automation transitions for long-term success.
Kawasan Industri Jababeka Tahap 1, Jl. Jababeka II D Blok C14L Cikarang, Indonesia (17530)
(021) 893 5060 Google Maps
Rungkut Industri III, No. 37, Rungkut Menanggal, Kec. Gn. Anyar Surabaya, Indonesia (60293)
(031) 9985 8624 Google Maps